How to Choose the Right Turning Tool Holder for CNC Machining
Understand the important factors for selecting a turning tool holder, including machine compatibility, insert geometry, clamping, rigidity, tool overhang, workpiece material, and CNC machining conditions.
 tosohex
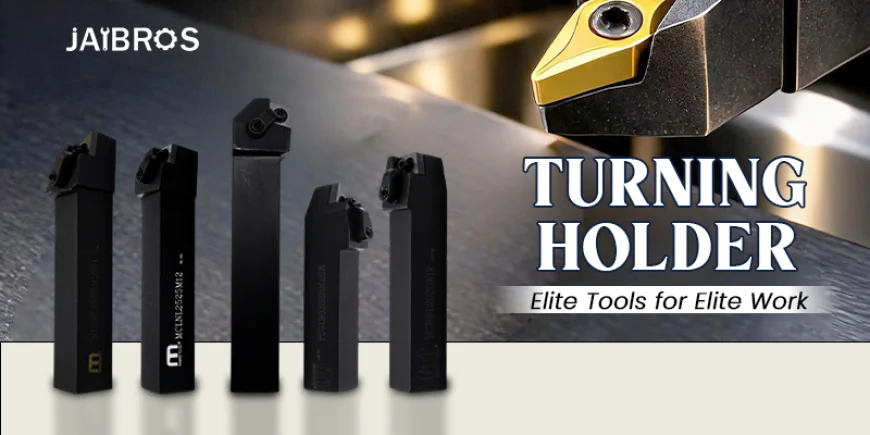
Selecting the proper Turning Tool Holder is very crucial for having successful CNC turning. The Turning Tool Holder links the cutting insert to the turret of the machine and makes sure that the cutting insert is positioned correctly in the process of machining. The proper tool holder will assist in vibration control, dimensional stability, surface finish, and protection of the cutting insert. Yet selecting the proper tool holder is not all about selecting the correct size. There are some other issues that should be considered prior to doing so.
This guide explains factors involved in choosing tooling for CNC turning. It covers machine compatibility, holder geometry, insert matching, tool overhang, workpiece material, cutting conditions, and clamping requirements. Understanding these areas makes selection systematic and helps create a setup.
1. Identify the Machining Operation
The first factor to consider is the type of CNC turning operation being performed. Different operations create different cutting forces and require different levels of clearance and tool support. Roughing, finishing, facing, profiling, grooving, and threading may therefore require different holder configurations.
Key Points:
-
Roughing requires strong support for higher cutting forces.
-
Finishing requires good stability for consistent surface quality.
-
Facing needs sufficient clearance around the workpiece.
-
Profiling requires suitable access to different workpiece contours.
-
Internal turning needs adequate reach without unnecessary overhang.
-
Threading and grooving generally require application-specific tooling.
A CNC Turning Tool Holder should therefore be selected according to the actual operation rather than using the same setup for every machining task.
2. Check Machine and Turret Compatibility
Machine compatibility should be confirmed before considering other holder characteristics. CNC lathes can have different turret designs, tool stations, mounting arrangements, and allowable tool dimensions. A holder that does not match the machine cannot provide a dependable machining setup, regardless of its cutting capability.
Key Points:
-
Check the required shank dimensions.
-
Verify the turret and tool station configuration.
-
Confirm right-hand or left-hand orientation.
-
Check the maximum permitted tool dimensions.
-
Make sure there is enough clearance around the chuck and workpiece.
-
Follow the machine manufacturer's tooling specifications.
The CNC Tool Holder arrangement must also match the machine's mounting system. Correct dimensional compatibility helps prevent installation problems and supports repeatable tool positioning.
3. Evaluate Holder Geometry and Rigidity
Holder geometry determines how the cutting insert approaches the workpiece and how much clearance is available during machining. Rigidity is equally important because cutting forces can cause vibration or deflection when the setup is insufficiently supported. The holder should provide the required access while maintaining adequate stability.
Key Points:
-
Match holder orientation with the cutting direction.
-
Select geometry suitable for the required machining profile.
-
Ensure adequate clearance between the holder and workpiece.
-
Avoid unnecessary tool projection.
-
Consider rigidity when performing heavy cutting.
-
Match the holder geometry with the insert shape.
A rigid Turning Tool Holder can help minimize unwanted movement during machining. However, maximum rigidity should not compromise access to the cutting area.
4. Match the Holder With the Insert
The insert and holder should always be considered as a combined tooling system. Their dimensions, seating arrangement, clamping method, and geometry need to correspond correctly. A mismatch can prevent proper seating and may result in inconsistent cutting performance or premature insert wear.
Key Points:
-
Check the insert shape and size.
-
Verify insert thickness and seating requirements.
-
Confirm the clamping mechanism.
-
Match the insert with the holder orientation.
-
Select a suitable insert grade for the workpiece.
-
Consider the appropriate chip-breaker for the operation.
When choosing a CNC Turning Tool Holder, the insert specifications should be checked at the same time. Different materials such as steel, stainless steel, aluminium, and cast iron can require different insert geometries and cutting conditions.
5. Consider Tool Overhang and Accessibility
Tool overhang describes the distance between the clamping point and the cutting edge. Excessive projection can reduce rigidity and increase the possibility of vibration or deflection. At the same time, the tool needs enough reach to access the required machining area, so overhang should be determined according to the workpiece geometry.
Key Points:
-
Keep tool projection as short as practical.
-
Maintain sufficient clearance around the workpiece.
-
Avoid unnecessary extension during external turning.
-
Allow additional reach only when the machining area requires it.
-
Pay particular attention to deep internal operations.
-
Check the complete setup for possible interference.
The Turning Tool Holder for CNC Machining should provide sufficient accessibility without creating unnecessary flexibility. A balanced setup can help maintain dimensional consistency and cutting stability.
6. Consider Workpiece Material and Cutting Conditions
Workpiece material directly affects cutting forces, heat generation, insert wear, and machining behaviour. A holder used for heavy steel roughing may need different stability considerations from one used for light finishing on aluminium. Cutting speed, feed rate, depth of cut, and coolant conditions should therefore be considered together with the tooling.
Key Points:
-
Consider material hardness and machinability.
-
Check recommended cutting speeds and feed rates.
-
Select insert geometry according to the application.
-
Consider the depth of cut and cutting forces.
-
Use coolant when required by the machining process.
-
Provide adequate rigidity for heavier operations.
Understanding these conditions helps ensure that the selected tooling is appropriate for the complete machining process rather than only the insert or holder dimensions.
7. Check Clamping and Maintenance Requirements
Clamping reliability and regular maintenance are important for maintaining consistent tool positioning. Chips, dirt, damaged seating surfaces, or loose clamping components can affect the position of the insert. Proper inspection and cleaning should therefore be part of routine CNC tooling maintenance.
Key Points:
-
Clean the insert seat before installation.
-
Inspect screws and clamping components regularly.
-
Check locating surfaces for damage.
-
Use the recommended tightening procedure.
-
Replace damaged components when required.
-
Store tooling in a clean and protected area.
A Turning Tool Holder should remain clean and properly maintained throughout its service life. Regular inspection can help prevent avoidable machining problems and maintain repeatability during tool changes.
Conclusion
The selection of tooling for CNC turning needs to take into account the entire machining process. Type of operation, machine compatibility, holder characteristics, insert characteristics, stiffness, tool stick-out, work material, cutting parameters, and clamping method may all affect the performance of the machining operation. Rather than choosing a holder based solely on size and price, these aspects should be taken into account based on the application.
A Turning Tool Holder for CNC Machining should ideally give the best positioning and stability for a particular operation. Jaibros can be one of the suppliers to consider when looking for CNC machining tools and accessories.
FAQs
1. What is the purpose of a turning tool holder?
It supports the cutting insert and connects it to the CNC machine's turret. Its purpose is to maintain the required cutting position during machining.
2. How can I check whether a holder fits my CNC lathe?
Check the machine documentation for turret dimensions, tool station type, mounting arrangement, shank dimensions, and maximum allowable tool projection.
3. Does holder rigidity affect surface finish?
Yes. Insufficient rigidity can increase vibration and tool deflection, which may negatively affect surface finish, dimensional accuracy, and insert life.
4. Can one holder be used for different turning operations?
Not always. Different operations can require different orientations, clearances, insert geometries, and clamping arrangements. The holder should match the specific application.
5. Why is tool overhang important?
Excessive overhang can increase deflection and vibration. Keeping the cutting tool as short as practical generally improves stability while still allowing sufficient access to the workpiece.