Resource Recovery Through Efficient waste management in brisbane
Upgrading local processing capabilities helps regional enterprises comply with strict state environmental regulations, decrease carbon emissions, and build a resilient circular economy.
 Ogtec
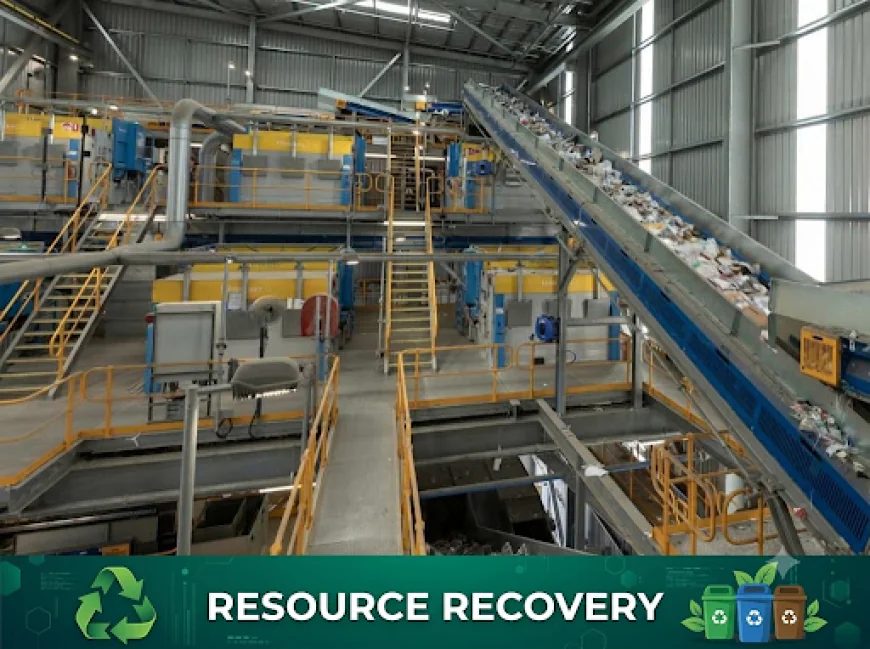
Rapid urbanization and expanding industrial operations across Queensland require advanced material recovery infrastructure to keep pace with municipal sustainability targets. Commercial facilities, manufacturing plants, and recycling hubs must adopt scalable processing frameworks to divert valuable resources from landfills. Implementing a structured waste management in brisbane strategy allows regional operations to process high volumes of commercial, industrial, and construction materials safely. Incorporating automated sorting technologies and high-capacity shredders lowers operational expenditures while enhancing overall material recovery rates. Upgrading local processing capabilities helps regional enterprises comply with strict state environmental regulations, decrease carbon emissions, and build a resilient circular economy.
Essential Components of High-Throughput Recycling Operations
Modern recovery plants rely on integrated mechanical systems to process mixed waste streams into clean, segregated commodities ready for remanufacturing. Implementing automated separation hardware eliminates processing bottlenecks and maximizes end-product purity.
-
Heavy-Duty Industrial Shredders: Reduce bulky materials, timber, and commercial waste to uniform sizes for efficient downstream sorting.
-
Air Density Separators: Use controlled airflow to isolate light fractions like plastic film and paper from heavy aggregates.
-
Trommel and Vibrating Screens: Classify mixed materials by particle size to protect delicate optical components.
-
Magnetic and Eddy Current Separators: Extract ferrous and non-ferrous metals rapidly without manual intervention.
Deploying comprehensive waste management in Brisbane solutions ensures that high-volume processing facilities maintain continuous operational throughput while meeting strict environmental standards.
Advanced Technology Integration for Industrial Waste Streams
Optimizing High-Volume Industrial Waste Management
Processing complex commercial and manufacturing waste streams requires heavy-duty machinery engineered to handle abrasive materials without excessive mechanical wear. Transitioning to integrated industrial waste management frameworks allows facility managers to process mixed plastics, metals, and construction debris efficiently.
Streamlining Operations with Automated Waste Sorting Systems
Incorporating state-of-the-art waste sorting systems improves sorting accuracy and reduces manual labor requirements. Optical sorters, ballistic separators, and robotic picking arms work together to increase secondary material recovery rates.
Maintaining Material Quality Through Contamination Control
Effective contamination control helps industrial facilities recover recyclable materials that meet downstream processing requirements. Removing hazardous items, excessive moisture, food residue, and non-recyclable contaminants before processing can reduce equipment damage and improve the quality of recovered materials. Regular inspections, waste stream audits, and monitoring of sorted outputs help operators identify separation problems early and maintain consistent material quality. These measures also support safer handling practices and reduce the amount of potentially recoverable material rejected during recycling.
Custom Mechanical Engineering and Long-Term Value
Every recycling facility faces unique spatial constraints, throughput demands, and material input profiles. Implementing tailored waste equipment solutions guarantees that shredders, screeners, and conveyors operate at maximum mechanical efficiency within existing plant layouts.
Custom-engineered processing lines optimize power consumption, streamline maintenance access, and adapt dynamically to shifting market demands for recycled commodities. Robust structural engineering ensures equipment longevity under continuous multi-shift usage.
Environmental and Economic Benefits of Modern Recycling
Upgrading processing infrastructure delivers tangible financial and environmental advantages to regional communities. Diverting high volumes of commercial and construction waste away from local landfills preserves valuable land resources and reduces greenhouse gas emissions. Efficient waste management in Brisbane frameworks helps commercial operators maintain compliance with regional environmental mandates while improving resource efficiency. Reliable machinery minimizes unexpected system halts and protects profit margins.
Advanced separation technologies produce high-purity recycled commodities that fetch premium prices in manufacturing supply chains. Investing in modern recovery technology strengthens supply chain resilience and fosters long-term regional economic growth.
Conclusion
Building a sustainable, low-carbon future depends on establishing efficient resource recovery infrastructure across commercial and industrial sectors. Partnering with experienced engineering specialists like OGTEC ensures access to custom plant designs, robust machinery, and reliable ongoing technical support. Implementing state-of-the-art separation and shredding systems lowers operational costs, enhances material recovery rates, and protects surrounding environments. Modernize your processing facility today to lead the shift toward a cleaner, more sustainable circular economy.