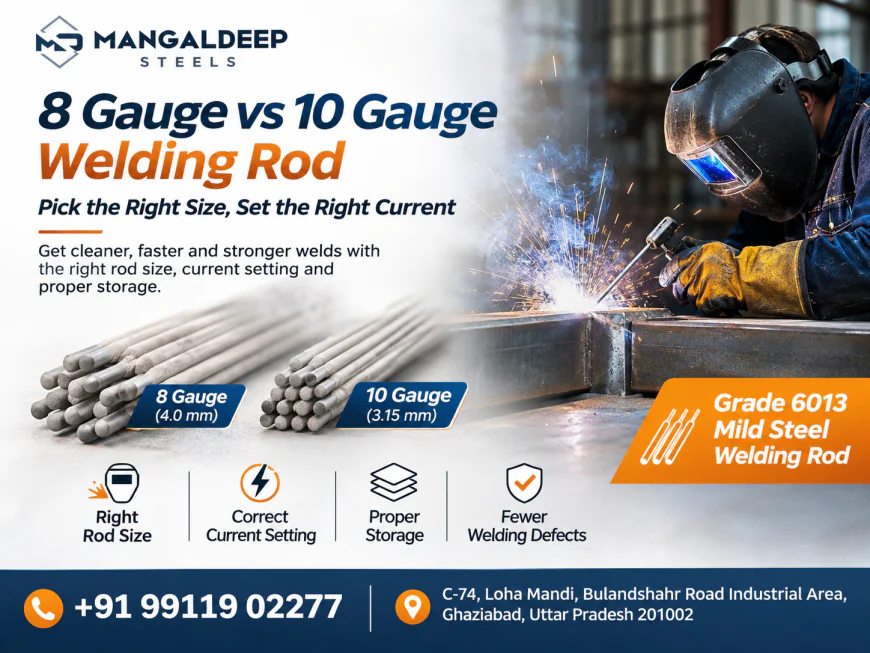
8 Gauge vs 10 Gauge Welding Rod: Pick the Right Size, Set the Right Current
Learn the difference between 8 Gauge and 10 Gauge Welding Rods, including sizes, current settings, applications, storage tips and common welding defects. Choose the right Mild Steel Welding Rod for cleaner and stronger welds with Mangaldeep Steels.
 Mangaldeep Steel
Most bad welds are not caused by bad welders. They come from the wrong rod size, the wrong current or damp rods. Fix these three things and your welds get cleaner, faster and stronger.
This guide covers rod sizes, current settings, storage and the most common defects with a Mild Steel Welding Rod.
Understanding 8 Gauge and 10 Gauge Welding Rod Sizes
In India, welding rods are commonly sold by SWG (Standard Wire Gauge) sizes. A lower gauge number indicates a thicker welding rod. The 8 gauge and 10 gauge rods differ in core diameter, current requirements and the thickness of steel they are suitable for.
1. 10 Gauge Welding Rod (3.15 mm)
A 10 gauge welding rod has an approximate core diameter of 3.15 mm and typically operates at 80–130 A when using an E6013 electrode. It is suitable for steel thicknesses of approximately 3–6 mm and is commonly used for welding gates, grills, furniture and frames.
2. 8 Gauge Welding Rod (4.0 mm)
An 8 gauge welding rod has an approximate core diameter of 4.0 mm and typically operates at 120–180 A when using an E6013 electrode. It is suitable for steel thicknesses of approximately 6 mm and above, making it useful for welding sheds, heavier frames and machine bases.
Important: These current ranges are starting points. Always check the manufacturer's recommended settings on the rod box and adjust the current according to the welding position and joint type.
How to pick the right size in 10 seconds
• Thin sheet or tube? Use 10 gauge at the lower end of the range to avoid burn-through.
• Thick plate or heavy angle and channel? Use 8 gauge for faster filling and good penetration.
• Overhead or vertical welds? Drop one size or lower the current for better control.
Storage: keep your rods dry
E6013 rods are more forgiving with moisture than low-hydrogen rods, but they still need care.
1. Keep boxes sealed until you need them.
2. Store off the floor, in a dry room, away from water and open doors.
3. Take out only what you need for the shift.
4. Do not use rods with cracked or flaking coating.
5. If rods get damp, dry them gently as advised by the manufacturer. Do not overheat, or the flux can fall off.
Common Welding Defects and How to Fix Them
Welding defects can occur due to incorrect current settings, damp welding rods, improper technique or poor surface preparation. Understanding the common problems and their causes can help you achieve cleaner and stronger welds.
1. Welding Rod Sticking to the Job
-
Likely Cause: Welding current is too low or the rod is damp.
-
Quick Fix: Increase the current slightly and use dry welding rods.
2. Excessive Spatter
-
Likely Cause: Welding current is too high or the arc length is too long.
-
Quick Fix: Reduce the current and maintain a shorter arc.
3. Porosity (Pin Holes)
-
Likely Cause: Damp welding rods or rust, oil and paint on the steel surface.
-
Quick Fix: Use dry rods and clean the joint until you reach bright, clean metal.
4. Undercut Along Edges
-
Likely Cause: Excessive welding current or an incorrect rod angle.
-
Quick Fix: Reduce the current and adjust the electrode angle and welding speed.
5. Slag Stuck in the Weld
-
Likely Cause: Poor cleaning between welding passes.
-
Quick Fix: Remove slag using a chipping hammer and wire brush before starting each pass.
6. Burn-Through on Thin Sheets
-
Likely Cause: Using a welding rod that is too thick or setting the current too high.
-
Quick Fix: Use a 10 gauge welding rod at a lower current to reduce the risk of burn-through.
Tip: Always select the correct welding rod size, maintain suitable current settings and keep your electrodes dry to minimise common welding defects.
A quick pre-weld checklist
☐ Correct rod size for the steel thickness
☐ Current set as per the rod box
☐ Rods dry, coating intact
☐ Joint cleaned of rust, oil and paint
☐ Earth clamp fixed close to the joint
Order Grade 6013 Mild Steel Welding Rod from Mangaldeep Steels
We supply Grade 6013 Mild Steel Welding Rod in 8 gauge and 10 gauge, rutile-coated, in boxes, with pan-India delivery. They strike easily, run on AC and DC machines, weld in all positions and leave a neat bead that needs little grinding before painting.
Welding gates, sheds, racks or machine frames? Buy your rods together with your steel channels, plates and angles from one supplier with over 30 years of experience. Call +91 99119 02277, email [email protected], or ask for a bulk quote.
FAQs
1. What is the size of a 10 gauge welding rod in mm?
About 3.15 mm core diameter.
2. What is the size of an 8 gauge welding rod in mm?
About 4 mm core diameter.
3. How many amps for a 3.15 mm 6013 rod?
Usually around 80–130 A. Check the box and adjust for position.
4. Why does my welding rod keep sticking?
The current is often too low, or the rod is damp. Raise the current slightly and use dry rods.