Getting Compressed Air Right for Abrasive Blasting
Getting Compressed Air Right for Abrasive Blasting
 Habib Nawaz
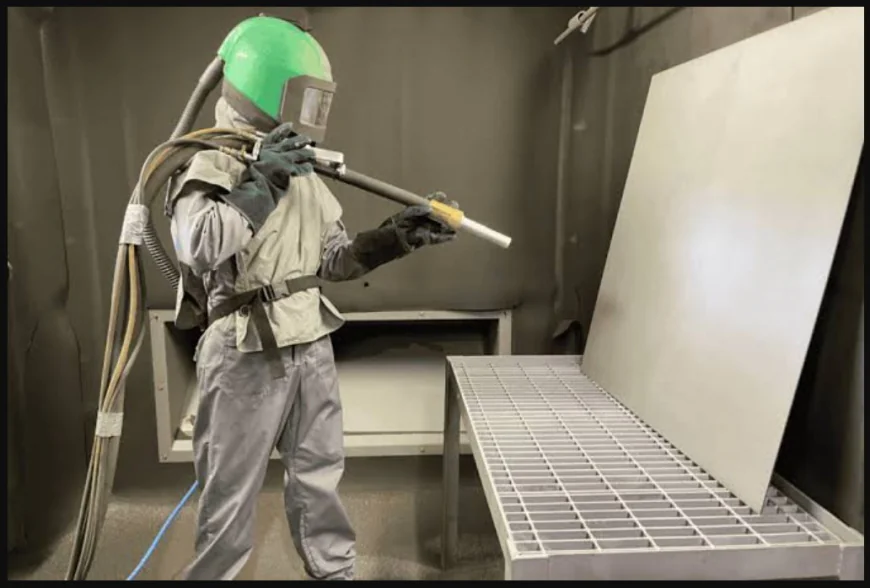
Abrasive blasting is one of the most demanding duties you can put on a compressed air system. A blast nozzle is, in effect, a continuously open hole that consumes enormous volumes of air for hours at a time, and the quality of that air shows up directly in the finish. Undersize the supply or let moisture through, and the symptoms arrive fast: slow production, blotchy profiles, flash rust, and a blaster who spends more time waiting than working. Getting the air right is what separates a blasting operation that runs all shift from one that stalls.
Nozzle Size Sets Everything
The single most important number in a blasting setup is the nozzle. As the nozzle wears, its bore grows, and a larger bore passes more air at any given pressure. A nozzle that has opened up through normal wear can demand dramatically more air than its original size, which is why a system that was adequate a few months ago can suddenly feel starved. The supply has to be matched to the worn nozzle the crew is actually using, not the new one in the box.
Pressure matters as much as volume. Blasting efficiency climbs steeply with nozzle pressure, so a few units of pressure lost to an undersized hose or a sagging supply translate into a noticeable drop in production. The target is to hold full working pressure at the nozzle while it runs continuously, which means the air source has to deliver both the volume and the pressure without fading as the receiver draws down.
Sizing the Air Source
Fixed plant compressors sometimes feed a blast booth, but much blasting happens outdoors, on remote structures, or at sites with no suitable permanent supply. That is where a portable air compressor sized for the job earns its place, bringing high continuous volume to the work rather than running long hoses back to a building. The key word is continuous: blasting is a steady, hours-long draw, so the machine has to be rated for sustained full-flow operation, not short bursts.
Sizing starts from the worn nozzle demand plus a margin for hose losses and any secondary air the operation uses, such as a blast helmet feed. Err toward headroom. A source running flat out at its limit all day runs hot and leaves nothing in reserve when a second nozzle comes online, while a source with margin holds pressure and runs cooler.
Moisture Is the Enemy of a Good Finish
Nothing ruins a blast profile faster than water. Moisture in the air stream clumps the abrasive, chokes the flow, and lays down humidity on the freshly cleaned steel that triggers flash rust before the coating ever goes on. In a Prairie climate, where humidity and temperature swing hard, dry air is not a luxury for blasting; it is a requirement for a surface that will hold paint.
An aftercooler and separator knock out the bulk liquid, but for a consistently dry blast stream, a desiccant dryer that holds a low dew point is what keeps moisture off the work in changing conditions. The payoff is visible: cleaner abrasive flow, a steadier profile, and far less rework from flash rust between blasting and coating.
Keeping the System Running Through the Shift
Blasting is hard on the whole air train. Abrasive dust and the sheer volume of air moving through the system load up filtration quickly, and a clogged filter steals pressure right where you can least afford it. Staying ahead of the filters and wear parts keeps pressure at the nozzle where it belongs and prevents the slow, creeping loss of production that comes from restricted air. A blasting operation that tracks filter condition and nozzle wear as routine maintenance simply gets more done between stoppages.
Heat is the other uptime factor. A compressor working at full flow in summer sun needs its cooling kept clear, because a unit that overheats and derates in the middle of a shift takes the whole crew down with it. Shade, airflow around the machine, and clean coolers are not details; they are what keeps the air on.
Matching the Supply to the Operation
Every blasting operation is a little different: nozzle count, duty hours, how remote the site is, and how demanding the coating specification is all change the right answer. The team at CFM Air Equipment works through those variables to match a supply, drying, and filtration package to the actual work rather than a generic flow figure. CFM Air Equipment also sees the common trap of a crew nursing a worn nozzle on a source that was right for the nozzle two sizes ago, and solving that early keeps a job on schedule.
Frequently Asked Questions
Why does my blast air seem weaker than it used to? The most common reason is nozzle wear. As the bore opens up it demands more air, so a supply that once held full pressure begins to sag. Measure pressure at the nozzle and check the bore before assuming the compressor has failed.
How much air does blasting really need? Far more than most point-of-use tools, and continuously. Size the source from the worn nozzle demand plus margin for hose losses and any helmet or secondary air, and favour headroom so the machine is not pinned at its limit all shift.
Do I really need a dryer for blasting? Yes, if you care about the finish. Moisture clumps abrasive and triggers flash rust on freshly cleaned steel. A desiccant dryer that holds a low dew point keeps the stream dry through changing weather.
Why does my filtration clog so fast during blasting? Blasting moves large volumes of air and generates dust, which loads filters quickly. Clogged filters drop pressure at the nozzle, so filter condition needs to be checked far more often than on a light-duty system.
Can one portable compressor run two nozzles? Only if it was sized for both running at once, including their worn bores. Adding a second nozzle to a source chosen for one will usually pull pressure down and slow both operators, so plan the capacity up front.