Reading a Bead Mill Specification Sheet Without Being Misled
Reading a Bead Mill Specification Sheet Without Being Misled Vendor specification sheets are written to describe a machine, not to qualify it for your application. The gap between those two things is where most purchasing mistakes live. A mill can be genuinely excellent equipment, correctly described, and still be wrong for the work you have — because the sheet reports capability while your process requires throughput, and those are differe
 johnmin ren

Reading a Bead Mill Specification Sheet Without Being Misled
Vendor specification sheets are written to describe a machine, not to qualify it for your application. The gap between those two things is where most purchasing mistakes live. A mill can be genuinely excellent equipment, correctly described, and still be wrong for the work you have — because the sheet reports capability while your process requires throughput, and those are different numbers.
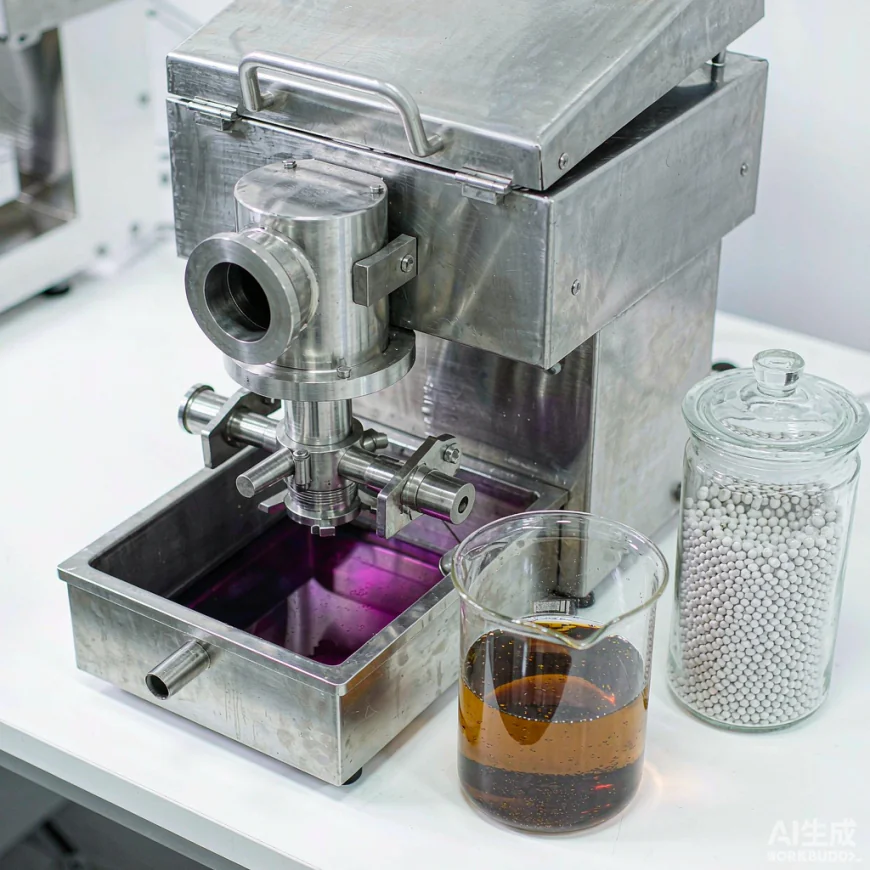
Having sat through many of these conversations from both sides of the table, the failures cluster into a predictable set. Below are the specification lines that matter, the questions that expose them, and the arithmetic that converts a spec sheet into a real production estimate. The reference machine throughout is a modern Laboratory Bead Mill covering the 2–10 litre class, where every one of these gaps becomes immediately visible because the batch is small enough to reason about precisely.
The Batch Volume Figure Is Doing More Work Than It Appears
Every useful wet milling specification states a batch range — for bench equipment, typically 2 to 10 litres per batch. Vendors quote this because it defines the machine's envelope. Buyers often skim it because it looks like a specification rather than a constraint.
It is worth pausing on what a properly stated batch range signals about the manufacturer. A supplier who publishes 2–10 litres has run product across that range. A supplier who quotes a single figure has run one point in it. On a Laboratory Bead Mill the honest version of this question is simply: at what batch volumes has this machine actually been run, and by whom.
In practice the number determines three other things that are frequently absent from the sheet.
Installed power versus batch mass. A fixed drive power spread across 2 litres produces a very different specific energy profile than the same power across 10 litres. The smaller batch runs hotter per unit volume, and the cycle time does not scale linearly with batch size. Doubling the batch does not halve the time; there is a fixed overhead in chamber loading, spindle spin-up and discharge that is amortised across the batch.
Contamination budget. In a 2 litre batch, even trace wear is a measurable fraction of the product. The same wear in a 200-litre production batch is negligible. If your specification is contamination-critical, the small-batch figure is the one that governs your material selection, not the large-batch figure.
Thermal headroom. Small batches heat faster and cool slower, relative to their mass. A machine that comfortably handles its rated batch at ambient will struggle with a viscous formulation in that batch. This is why viscosity, not volume, is often the real constraint in bench work.
So the batch range is not a single specification among many. It is the key that unlocks the interpretation of the others.
Power Figures Are Peak Ratings, Not Working Figures
Installed motor power is the easiest number on the sheet and one of the most frequently misused. It represents the peak the drive can deliver, not the power the process can absorb.
On a small chamber the gap between the two can be substantial. A drive rated for its peak will still slow under a dense ceramic charge in a viscous batch, and when it slows, the batch temperature rises, which raises the viscosity further. The system finds a stable but unsatisfactory operating point, and the cycle takes longer than the sheet suggests.
Two questions separate the two numbers in practice. Ask what the speed is under load rather than no-load. And ask whether the machine maintains rated speed through the discharge phase, or whether it slows as the chamber empties. On a well-designed lab-scale bead mill the answer to the second question is yes, and that is a design feature worth paying for.
There is a related question about the drive that is almost never asked: does the machine derate on start-up, or does it attempt full speed immediately against a stationary charge? Immediate full speed against a settled ceramic bed is a shock load on both the media and the drive train, and it is one of the reasons chamber design and drive control cannot be evaluated independently of each other. A Laboratory Bead Mill that ramps into speed takes noticeably longer to reach the plateau, and that is the correct behaviour rather than a slow machine.
Noise as an Engineering Indicator
A published noise figure in decibels looks like a compliance line item. It is actually one of the most informative engineering indicators available, and it is worth reading carefully.
Noise in a bead mill comes from bead-on-bead collision, bead-on-chamber impact, and the drive train. The first two are design outcomes. A well-designed chamber has controlled bead loading geometry and a wall profile that does not reflect collision energy back into the charge. A poorly designed one does not, and the difference is audible.
A specification stating under 65 dB is therefore a claim about chamber design, not merely about acoustic output. If the sheet omits the figure entirely, that is a reasonable inference too — though it is a weaker signal than an explicit bad number.
The practical check costs nothing: run the unit at full speed with a realistic charge in the room it will actually occupy, and listen. A machine that will not be usable in the space it is sold for is not a machine that will get used properly in that space.
Wetted Materials, and Where Metal Creeps In
Ceramic wetted parts are standard for good reason, and the reason is arithmetic rather than marketing. When the batch is 2 litres, a few milligrams of metallic wear debris from a steel screen holder is not trace contamination — it is a measurable concentration in the finished product.
The specification sheet will typically state the primary wetted materials. What it usually omits are the secondary and tertiary components: the screen holder, the fasteners in the discharge path, the seal faces, the shaft coupling. These are exactly where metal finds its way into a product that was processed in a ceramic chamber with ceramic media.
Three questions close the gap. Which materials contact the product, specifically including the discharge path. Whether any fastener or seal in that path is metal. And whether the screen itself is a wetted component or is isolated behind a ceramic carrier. On a machine designed for pigment and battery-material work, the answers should all be ceramic or equivalent; on a general-purpose machine, they usually are not.
Structure: The Split Chamber Is a Process Decision
Whether the chamber opens horizontally or is accessed vertically is listed as a structural feature. In a development laboratory it is a process decision with direct consequences for data quality.
A horizontal split chamber lets you reach the media bed, the screen and the chamber walls in one operation, and lets beads drain from the side. That makes fast, complete cleaning possible between samples — and cleaning speed determines how many independent runs a screening programme can afford, which in turn determines how much of the dataset is genuinely independent rather than a series of partially contaminated repeats.
On a vertical closed chamber, the same cleaning is a disassembly job with more steps and more opportunity for variation in reassembly. Over a long campaign, that difference accumulates into a measurable drift in results.
This matters most for development work and least for repetitive production work, which is why the same machine can be right for one lab and wrong for another.
What the Sheet Does Not Tell You, and Must Be Asked
Filtration. What screen sizes are available, what the pressure drop is at realistic flow, and whether the screen carrier is a consumable. On small batches the filter is a process variable, not an accessory.
Media range. Which bead diameters are available for the chamber, and whether graded charges are supported. A machine with a narrow media range constrains your entire process design.
Cooling. Whether the chamber can be jacketed, and whether temperature is measured. This determines whether you can generate data that transfers to production or only data that is thermally limited to the bench.
Clean-down time. Ask for it, then verify it yourself with a timer. It is a claim, and like all claims it is easiest to evaluate in your own space.
Converting a Sheet Into an Estimate
Once you have the specific energy figure and a validated cycle time on your own material, real throughput follows from arithmetic rather than from optimism.
Take your cycle time, subtract the fixed overheads (charging, spin-up, discharge, cleaning amortised), divide the remainder by the batch volume, and apply a realistic availability figure. Availability on bench equipment in a busy laboratory is often 40 to 60 percent rather than the 80 percent a vendor calculation assumes, because the machine competes for attention with everything else on the bench.
Run that calculation with a realistic availability number and it will change how you staff the work. It is the difference between a programme that produces twelve usable samples a week and one that assumes eighteen and plans accordingly.
Questions Worth Asking Before You Sign
What is the stated noise level under a realistic charge. Which wetted materials contact the product, including fasteners in the discharge path. What speed does the drive hold under load, not no-load. What is the published performance tied to, in terms of a stated batch volume. Which bead grades are available. How long does a complete clean-down take. Is temperature measured, and can it be controlled. And what does support look like after commissioning, specifically for spindle and controller service.
None of these questions is difficult to ask, and a supplier who answers them directly is telling you something about how they build machines. On a laboratory rod pin grinding configuration the specification envelope is where these conversations should start, because it establishes the machine class before any commercial discussion begins.
Summary
Read a specification sheet as a set of conditional claims rather than a list of capabilities. The batch volume determines power interpretation, contamination budget and thermal headroom. The power figure is a peak, not a working number. The noise figure is a proxy for chamber quality. The wetted material list is incomplete until you ask about fasteners. And the structure determines your data quality more than any other single feature. None of this is hidden from a careful reader — but almost none of it is volunteered either.