Nine Models from 0.5 to 1200 kg per Hour: the Selection Logic Behind the Range
The 300 and 320 share 45 kW of compressor power and differ by 50 kg/h, so a model number is not a capacity. How the nine-model ladder actually works, why adjacent models overlap, and how to pick.
 johnmin ren
Nine models from 0.5 to 1200 kg per hour: the selection logic behind the range
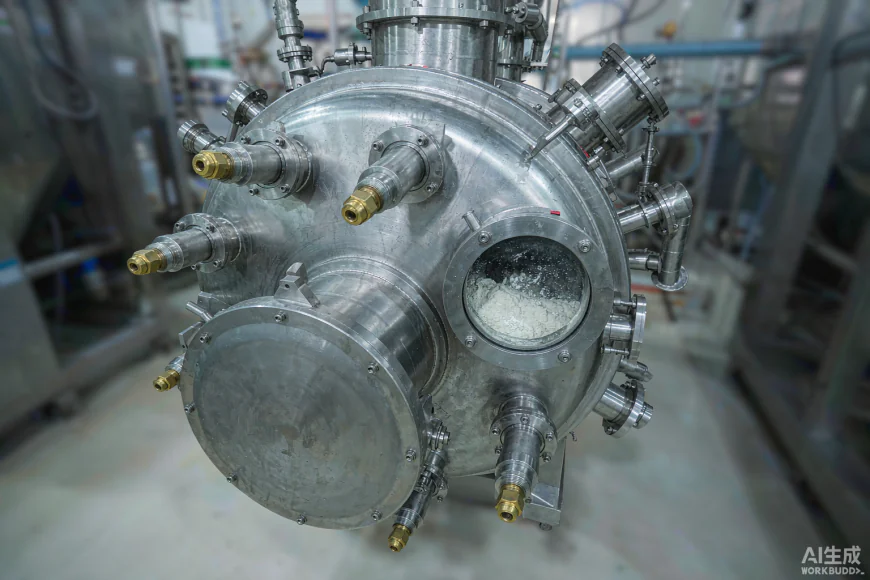
A model ladder is a catalogue convenience until you can predict which rung you need. This range is nine machines, designated 100, 200, 300, 320, 400, 500, 600, 700 and 800, spanning three and a half orders of magnitude in throughput from 0.5 to 1200 kg per hour. The useful question is not which model is most powerful, but which model your annual tonnage and shift pattern actually load.
The range as published
All nine models work at the same pressure envelope, 0.7 to 1.0 MPa, so pressure is a shared variable rather than a differentiator. What separates the models is air consumption, and through it compressor power, and through it throughput.
| Model | Working pressure (MPa) | Air consumption (m3/min) | Compressor power (kW) | Capacity (kg/h) |
|---|---|---|---|---|
| 100 | 0.7-1.0 | 1.2 | 11 | 0.5-20 |
| 200 | 0.7-1.0 | 2.7 | 22 | 0.5-50 |
| 300 | 0.7-1.0 | 5.2 | 45 | 10-100 |
| 320 | 0.7-1.0 | 5.5 | 45 | 10-150 |
| 400 | 0.7-1.0 | 7.7 | 75 | 20-200 |
| 500 | 0.7-1.0 | 10.6 | 90 | 50-300 |
| 600 | 0.7-1.0 | 17.5 | 132 | 100-500 |
| 700 | 0.7-1.0 | 30.7 | 250 | 300-800 |
| 800 | 0.7-1.0 | 41.4 | 500 | 600-1200 |
Two structural facts follow from that table, and both change how you read a quotation.
The first is that energy scales with throughput. Air consumption rises from 1.2 to 41.4 m3/min across the ladder and compressor power from 11 to 500 kW, close to proportionally. There is no energy economy of scale. Moving from the 500 to the 800 model does not buy a better watt-per-kilogram figure; it buys four times the compressor power, 3.9 times the air volume and four times the throughput.
The second is that the lower bound of capacity does not fall in proportion to the model number rising. The 100 and 200 models reach down to 0.5 kg/h. The 300 and 320 reach 10 kg/h. The 400 reaches only 20 kg/h, and the 800 will not go below 600 kg/h under any circumstances. A ladder that behaved intuitively would widen at the bottom as it widened at the top. This one narrows, and that is a design consequence rather than an omission.
The model number is not the capacity
The clearest evidence is the pair 300 and 320. They share 45 kW of compressor power. They share the 0.7 to 1.0 MPa working pressure. Their air consumption differs by about six per cent, 5.2 against 5.5 m3/min. And their published capacities are 10-100 kg/h and 10-150 kg/h. Two machines drawing essentially the same air deliver maximum throughputs that differ by fifty per cent.
If the model number carried throughput, that pairing would be impossible. The number identifies a machine configuration — nozzle geometry around the chamber wall, chamber volume, feed injector sizing — not a capacity figure. Reading 320 as "a larger 300" and expecting it to differ from the 300 in every other respect is the most common misreading of this ladder, and it produces a purchase sized on the wrong basis.
The practical consequence is that an Airflow Crusher has to be quoted against a duty rather than a model number. The quotation should name your material, feed size, target D50 and annual tonnes, and the supplier should commit to a capacity for that duty. The published range is a mechanical envelope, not a performance guarantee, and the gap between the two is where most capacity disputes originate.
Capacity is a range, and the range is the specification
Each figure is published as a range, and the bottom of that range carries as much information as the top. The 500 model is published at 50-300 kg/h, a factor of six between the extremes of one machine on one air supply. That spread reflects real variables: feed top size, size distribution, bulk density, cohesion, target fineness, and the pressure actually held at the manifold.
Two sizing errors follow from treating the upper bound as a rating. Sizing on 300 kg/h means running a machine at the edge of its envelope on day one, with no margin for a feed material change or a pressure shortfall. Sizing on 50 kg/h means buying several machines in parallel, multiplying footprint, ducting and control scope for no process benefit. The defensible number sits between the two and comes from a trial on your material.
Why adjacent models overlap
The overlap is systematic rather than accidental. The 300 and 320 both serve 10-100 kg/h. The 320 and 400 both serve 20-150. The 400 and 500 share 50-200, the 500 and 600 share 100-300, the 600 and 700 share 300-500, and the 700 and 800 share 600-800. Any duty in an overlap band can be served by either neighbour, which is why model selection cannot be reduced to matching one number against another.
Four criteria break the tie when two models both fit:
- Minimum acceptable rate. If your campaign must run at 8 kg/h, only models reaching below 10 kg/h are candidates, and that alone eliminates the 400 and everything above it.
- Headroom. At 150 kg/h required, the 320 sits at the very top of its range with no reserve; the 400 sits comfortably inside 20-200 kg/h.
- Air infrastructure. Moving up a rung costs air. The step from the 500 to the 600 is 6.9 m3/min and 42 kW. If the compressor house cannot absorb that, the tie is decided for you.
- Configuration scope. Higher models carry more nozzle positions and more chamber adjustment, which matters if you expect to change products later.
Where two models genuinely serve the same duty at the same headroom and air cost, take the smaller one. The larger machine gives no additional process capability and simply sits closer to its ceiling. This is the judgement that an Airflow Crusher selection normally turns on, and it is a judgement made on installed cost per usable kilogram rather than on headline capacity.
Sizing from annual tonnage and shift pattern
The calculation from a product volume figure is arithmetic, and it is where specifications most often go wrong. Take annual tonnes, divide by operating days and by hours per day, and you have the average kilograms per hour the plant must deliver. A 2400 tonne per year requirement running five days a week for eight hours a day is about 120 kg/h of real production time, and that is an average, not a machine size.
Apply two corrections. The first is a duty factor, typically 1.3 to 1.5 on the catalogue figure, because the published maximum assumes a free-flowing brittle feed of modest top size and pressure held at the top of the envelope. The second is redundancy: a single machine is a single point of failure for the whole production target, and for a colour, additive or pharmaceutical intermediate that is rarely acceptable commercially. Where the annual figure justifies it, two machines at roughly 60 to 70 per cent load each cost less in lost production than one at full load.
Duty cycle: batch and continuous
Shift pattern changes the answer more often than material does, because the two ends of the capacity range constrain different things. In batch work the constraint is the floor. A 200 kg colour concentrate campaign on a 400 model, whose lowest published rate is 20 kg/h, needs ten hours of milling. The same campaign on a 200 model, which reaches down to 0.5 kg/h, runs in five hours at 40 kg/h. The extra air and power of the larger machine are wasted for the whole campaign.
Continuous duty shifts the constraint to the ceiling and to thermal behaviour. A machine held at 120 kg/h continuously is a different duty from the same machine cycled to 150 kg/h for twenty minutes and then stopped, because sustained loading is what exposes an air supply that cannot hold pressure, a feed system that cannot deliver uniformly, and a discharge that restricts under continuous flow.
Changeover cost is also mechanism-dependent. Because there are no mechanical transmission parts inside the grinding chamber, there is no media circuit to drain and no seal to change between products. A batch sequence running four products a week is executed by opening the chamber, brushing it out and reassembling. That shortened interval is often the hidden constraint in contract manufacturing work, and it is one of the easier arguments to quantify for an Airflow Crusher in batch service.
The air supply decides before the model does
Compressed air is the only energy input, so installed air capacity can veto a model choice outright. The 800 model needs 41.4 m3/min at 0.7 to 1.0 MPa and a 500 kW compressor. On a site where a 250 kW compressor is already committed, that model is not a technical question. Conversely the 100 and 200 models need 11 and 22 kW, which is within reach of almost any plant and makes them genuinely portable development assets.
Air quality matters as much as quantity. The material is entrained and reduced in a dry gas stream, so moisture, oil carry-over and dew point are process variables rather than housekeeping items. Establish the measured dew point at the point of use, not at the compressor outlet, before the model is fixed.
A selection sequence that works
Run these in order and the model usually resolves itself without trialling every candidate.
- Confirm the material is a dry, free-flowing, brittle powder within the chamber lining's hardness limit.
- Calculate required average kg/h from annual tonnage, operating days and hours per day.
- Apply a duty factor of 1.3 to 1.5 and treat the result as the working point.
- Check the shift pattern. If batch work dominates, judge the working point against the minimum sustainable rate rather than the maximum.
- List every model whose published range brackets the working point, then apply the tie-break criteria above.
- Confirm the shortlisted model's air consumption and compressor power fit the site's installed capacity and treatment.
- Check the lining specification against the actual Mohs hardness of your hardest constituent.
Note that step six can eliminate the technically correct answer. Alumina ceramic lining suits material up to Mohs 8, which covers most minerals and pigments but not the top of the abrasive range. Fineness of D50 below 5 micrometres is achievable on appropriate feeds and the vertically adjustable discharge gives real control over where in the distribution you operate, but both depend on a feed that is dry, brittle and free-flowing. Once those two constraints are checked, the model ladder itself is the easy part of the decision.