First Article Approval Is a Contract, Not a Milestone
A first article report records a result. It does not record the conditions that produced it, and every assertion in it is conditional on fixture, parameters, material and equipment staying unchanged.
 johnmin ren
First Article Approval Is a Contract, Not a Milestone
Automation projects treat first article approval as a milestone: a date on a plan, a signature on a document, and a gate that the project passes through on the way to production. That framing is convenient and it is wrong in a specific way that costs money later.
First article approval is not a gate. It is a contract about what the process will do from then on. Everything the supplier asserts when they ask you to sign it is a promise about future output, and the useful question is not whether the part is acceptable but whether each assertion is one they can keep.
What is actually being signed
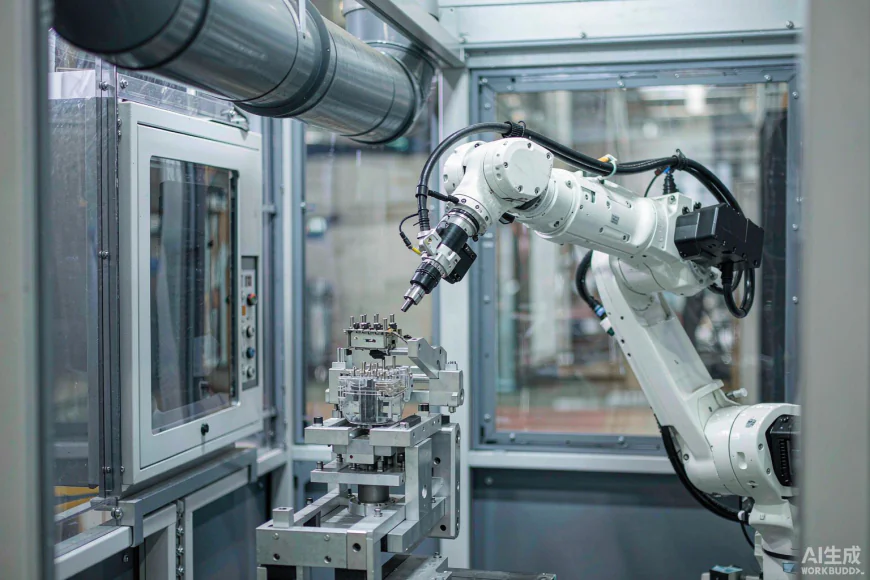
When an automated Laser Welding Cell is handed over, the first article package is a set of conditional assertions about future production. Reading them individually is the entire review.
When a supplier submits a first article for approval on an automated welding cell, a typical package contains more than a conforming part. It contains assertions, and they are worth reading individually.
The measured results, with the actual values rather than pass marks. This is the least contentious item and the most useful: a dimensional record showing where the part landed relative to every specified characteristic.
The process parameters used to produce it. A parameter list attached to a first article is a statement that this set of parameters produces this result. If the parameters are not recorded, the result is a coincidence rather than a specification.
The fixture identification. Which fixture, which revision, which locating scheme. A first article produced on a fixture that will be modified for production has approved a result that will not recur.
The material identification. Grade, specification, and where practical the heat or lot. On a welding process, material condition is part of the process, and a first article approved on one lot says nothing about another unless the process window is wide.
The equipment identification. Which cell, which source, which tooling. A cell that is subsequently reconfigured or has its source replaced is a different process.
Any concession granted, with the reason. This is the item most often missing and the most damaging, because an unrecorded concession becomes a tolerance that everybody believed was agreed and nobody can now evidence.
Which of those assertions can the supplier actually keep
This is the useful review, and it turns on asking a different question of each: is this a property of the part, or a property of the conditions?
A measured dimension on the first article is a property of one part. It is the weakest kind of evidence and it is treated as the strongest, because a number on a report looks conclusive. It tells you the process can produce a conforming part. It does not tell you it will produce only conforming parts.
A recorded parameter set with a demonstrated process window is a property of the process. It is stronger, because it survives a different part and a different operator. If the package includes the acceptable range rather than a single set, it is stronger again, and that is the single most valuable item in the document.
A fixture revision is a property of the tooling. It is stable until somebody changes it, which is exactly when you need to know it was recorded.
A material lot is a property of the supply. It is stable only if the supplier controls incoming material, which on a welding process is worth confirming rather than assuming.
An equipment identification is a property of the asset. Stable, and entirely dependent on nobody reconfiguring it without re-approval.
A recorded concession is a property of the agreement. It is the only item on the list that prevents a future dispute, and the only one that costs nothing to produce.
Approval language worth insisting on
Two clauses, both standard in a quality agreement and frequently absent from an automation handover document.
First, that approval is conditional on the identified fixture, parameters, material condition and equipment remaining unchanged. This is not distrust; it is the definition of what was approved. Without it, the approval is of a process nobody has described, and any later variation becomes a question of interpretation.
Second, that any change to those four items requires notification before implementation. The clause is simple and it is the one that gets discussed when it is too late rather than when it is drafted.
Neither clause is adversarial. Both exist because the assertions in a first article are conditional, and a conditional assertion that is not recorded as conditional becomes an unconditional one by default.
The measurement that should worry you most
On a welding cell there is usually one characteristic that dominates the risk, and it is worth identifying it explicitly rather than reviewing the whole report evenly.
It is frequently a mechanical property of the joint rather than a dimension — shear strength, pull-out strength, or a related figure. The reason is that the customer specification for an electrical connection is typically a mechanical one, while the first article report is typically dimensional. A report full of dimensional conformance can sit alongside a joint that is marginal on the property that actually matters.
If the specified characteristic is mechanical, the first article package should include a mechanical result. If it does not, that is a gap worth raising at approval rather than discovering at a field return, and it is a gap that no dimensional evidence substitutes for.
The second one worth watching is the position of the joint relative to its datum, measured after the part has been released from the fixture. A weld that lands correctly in the fixture and has moved after unclamping will pass a first article inspected in the fixture and fail a customer inspection on the bench.
What the production run should verify
On a Laser Welding Cell the useful verification is measured after the cell has been running normally, not in the first hour after approval when every consumable is fresh.
Approval should be followed by a defined production verification, and the number of parts in it is a decision worth making deliberately.
The useful content is not more dimensional reports. It is the characteristics identified as dominant, measured on parts produced after the cell has been running — after the nozzle has been changed, after the fixture has been cleaned, after a shift boundary. Parts produced in the first hour after approval are the least informative parts in the entire programme.
Five to ten parts taken after normal operating time, measured on the dominant characteristics, with the parameter records attached, is a verification that answers the only question the first article cannot: does the process hold.
The point worth putting in the handover meeting
First article approval is the moment where a project converts engineering effort into a production assumption. Everything before it was investigation; everything after it is production against that assumption.
The most common failure is not a defective part. It is an approval taken on a package that recorded a result but not the conditions that produced it, followed by six months in which every part is nominally to an approved process and no one can say what the approved process is.
For a Laser Welding Cell on a switch component programme, that risk concentrates in exactly one place: the process window. The cell will produce a conforming part on approval day. The question the approval should answer is whether it will produce conforming parts on day ninety, after the nozzle, the wire, the fixture and the material lot have all moved through their normal cycles.
A first article report that records a parameter set demonstrates a point in that window. A report that records the window demonstrates a process. Only one of them is a contract.