CNC Turning Center: How It Improves Modern Machining
When manufacturers compare turning equipment with alternatives such as a 5-axis vertical machining center, they should focus on the types of surfaces, features, and production sequences their components actually require.
 kathie walker
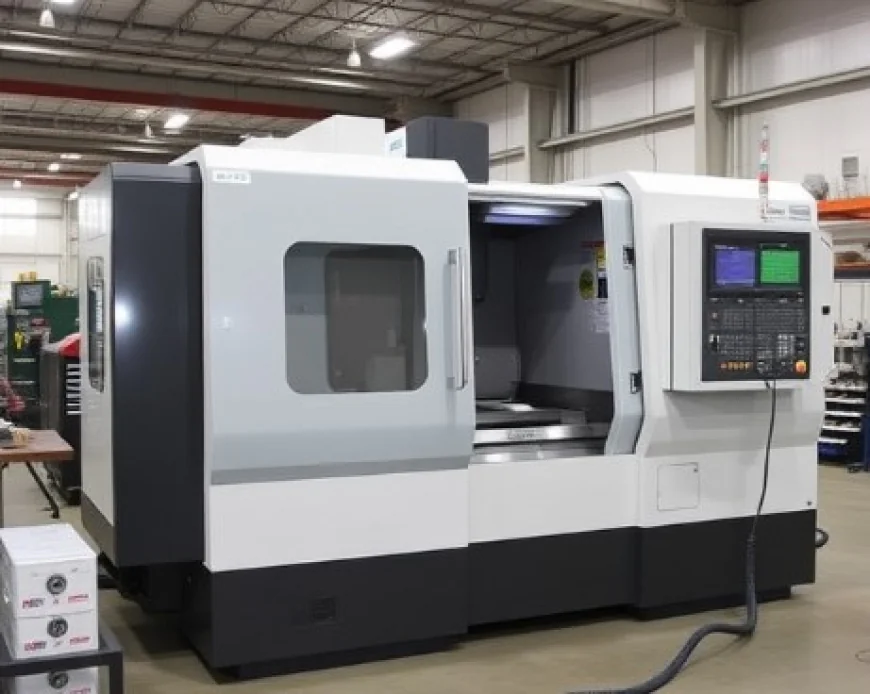
Modern manufacturers increasingly rely on computer-controlled equipment to produce components with consistent dimensions, repeatable results, and efficient cycle times. Among these systems, turning equipment has evolved considerably from conventional lathes. A CNC turning center combines automated control with advanced tooling and workholding capabilities, allowing manufacturers to perform multiple operations with greater consistency. Depending on the machine configuration, operations can include facing, threading, drilling, boring, grooving, and other cutting processes. Turning centers are particularly useful when production requires repeatable cylindrical or rotational features with controlled tolerances.
Understanding How Turning Centers Work
The fundamental principle remains similar to conventional turning: the workpiece rotates while a cutting tool removes material. However, CNC control coordinates spindle speed, feed rate, tool movement, and cutting sequences according to programmed instructions. The spindle axis is normally designated as the Z-axis, while radial movement is associated with the X-axis.
Modern CNC turning center configurations may include automatic tool changers, live tooling, multiple turrets, or sub-spindles. These additions can reduce the number of manual interventions and eliminate some secondary operations. Live tooling, for example, allows certain milling or drilling operations to be performed while the component remains secured in the machine, depending on the equipment configuration.
Key Operations Performed on These Machines
Turning centers can handle several machining processes. Facing creates a flat surface on the end of a rotating workpiece, while external turning reduces diameter or creates stepped profiles. Threading produces internal or external threads, and boring enlarges or refines existing holes. Drilling, grooving, parting, and chamfering are also common operations.
The ability to combine operations can be especially valuable for parts requiring several features. Instead of transferring a component between separate machines, manufacturers may complete more of the machining sequence in one setup. Fewer setups can reduce handling time and help limit errors associated with repeatedly repositioning the workpiece.
Selecting the Right Machine Configuration
Machine selection should begin with the geometry, material, dimensions, production volume, and required tolerances of the component. A basic two-axis turning configuration may be adequate for straightforward cylindrical parts, while more advanced equipment becomes useful when components require additional machining processes. When manufacturers compare turning equipment with alternatives such as a 5-axis vertical machining center, they should focus on the types of surfaces, features, and production sequences their components actually require.
Manufacturers producing complex components may also consider mill-turn equipment. These machines integrate turning with milling capabilities, potentially allowing multiple processes to be completed in one setup. Multi-axis systems can further improve access to angled or complex surfaces. However, additional axes also introduce greater programming, tooling, and maintenance considerations.
Production Benefits Beyond Basic Turning
A major advantage of a CNC turning center is repeatability. Once a validated program, tooling strategy, and workholding arrangement are established, the same machining sequence can be reproduced across production batches. Automated tool management and probing systems can further support process consistency where available.
Cycle time is another important consideration. Reducing workpiece transfers and combining operations can shorten overall production routes. In high-volume manufacturing, even small reductions in handling or setup time can influence total manufacturing costs.
Planning Investment and Long-Term Use
Purchasing CNC equipment requires more than comparing machine prices. Buyers should evaluate spindle capacity, axis travel, chuck or workholding requirements, tooling compatibility, control capabilities, automation options, service support, and expected production volume. Energy consumption, maintenance, operator training, and tooling expenses should also be included in the ownership calculation.
For businesses expanding machining capacity, CNC machine financing may be considered as part of an equipment acquisition strategy. Financing can help spread capital expenditure over time, but the decision should still be based on projected production requirements and total ownership costs.
Conclusion
Choosing appropriate CNC equipment requires a clear understanding of part geometry, production demands, material characteristics, tolerance requirements, and the number of operations involved. A properly specified turning system can improve repeatability, reduce handling, and support efficient production of rotational components. As manufacturing requirements become more complex, integrated equipment can also provide opportunities to combine turning, drilling, and milling processes. For operations that depend heavily on prismatic features rather than rotational work, a CNC milling machine may provide a more suitable machining approach. The key is matching machine capability with actual production requirements rather than selecting equipment based solely on its number of axes or headline specifications.