CNC Machining AZ80A Magnesium: Tooling, Speeds and Safety
Practical CNC machining notes for AZ80A magnesium: cutters, published starting data, workholding, chips, safety, inspection, and RFQ details.
 李志文
What a Machine Shop Needs to Know Before Cutting AZ80A Magnesium

AZ80A is usually selected for wrought magnesium parts that need a step up in strength. It shows up in extrusions, bar, forgings, and machined structural blanks. From the cutter’s point of view, the material removes easily. The job becomes less casual when the drawing includes thin webs, deep pockets, flatness requirements, or a lot of material coming off one side of the part.
The starting stock makes a difference. A compact AZ80A forging may stay put through aggressive facing and pocketing. A long extrusion can move once clamps are released, especially after a large cavity is machined near one edge. Shops see this all the time with lightweight parts: the dimensions are fine while the part is in the fixture, then the free-state measurement tells a different story.
That is why workholding and tool reach should be reviewed before the program is finished. Use stable datum surfaces. Support broad floors. Keep the cutter short where possible. A deep internal corner that forces a long, small-diameter end mill may slow the job down far more than the material itself. If the feature is not functional, a slightly larger internal radius can make the setup much friendlier.
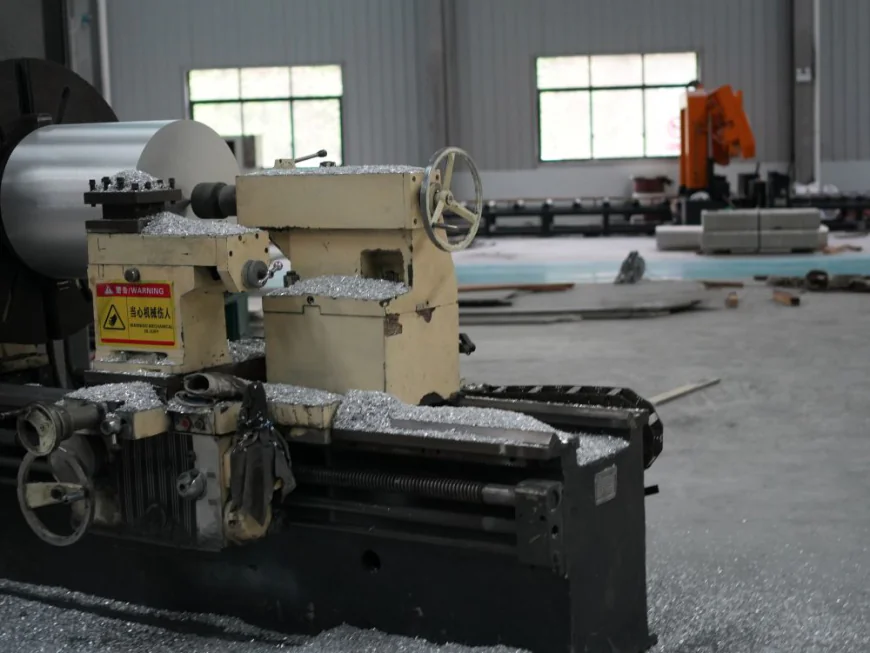
AZ80A also needs a sensible chip plan. Sharp carbide tooling and clear flute space help produce a clean cut. Letting a cutter rub on a thin wall creates heat and fine swarf, neither of which helps finish or process control. The shop’s approved method for chip collection, cleanup, cutting fluid, and fire protection matters just as much as the toolpath. Magnesium chips are combustible, so this is not a job for an improvised cleanup routine.
For buyers, the most useful items on the RFQ are the actual material form and condition, the areas that carry load or seal, free-state versus supported flatness where relevant, and the coating or fastener materials used later in assembly. Those details tell the supplier whether a simple fixture is enough or whether the part needs a more careful sequence of roughing, releasing, and finish machining.
If a part will be quoted by more than one supplier, ask whether each shop already has a documented process for magnesium chips. It is a practical screening question, and it often reveals more than a generic statement about CNC capacity.
For tooling references, published speed data, workholding notes, and magnesium safety considerations, see this CNC machining AZ80A magnesium guide.