How Do I Check Collet Runout With a Dial Indicator?
Learn how to check collet runout with a dial indicator, measure TIR, detect alignment issues, and improve machining accuracy.
 Aadarsh Sharma
In machining, even a small alignment problem can affect the final result. A tool that does not rotate evenly may leave a poor surface finish, reduce dimensional accuracy, and cause cutting tools to wear out faster. One common reason behind these problems is collet runout.
The good news is that checking collet runout does not have to be complicated. A dial indicator can help you measure how much a tool or test bar moves while rotating. With the right setup and a few simple steps, you can identify alignment issues and keep your machining operations running smoothly.
What Is Collet Runout?
Collet runout occurs when a tool or workpiece does not rotate perfectly around its central axis. Instead of staying evenly centered, it moves slightly from side to side as the spindle turns.
This movement may seem minor, but it can make a noticeable difference during precision machining. Excessive runout can cause vibration, uneven cutting, poor surface quality, and unnecessary tool wear.
Runout is commonly measured as total indicated runout (TIR). It is the difference between the highest and lowest readings recorded by a dial indicator during one complete rotation. The lower the reading, the less variation is present, although the acceptable limit depends on the machining application and equipment specifications.
What Do You Need to Check Collet Runout?
Before beginning the inspection, make sure you have the right tools ready. You will generally need:
- A dial indicator with suitable measuring accuracy.
- A rigid magnetic base or indicator stand.
- A clean precision test bar or cylindrical tool shank.
- A compatible collet and collet chuck.
- Cleaning materials to remove dust, oil, and metal chips.
A precision test bar is often a good choice because it provides a consistent surface for measurement. Make sure the indicator is in good condition and the machine components are clean before you start.
Step-by-Step Process for Checking Collet Runout
1. Clean the Collet and Spindle
Start by switching off the machine and following the required safety procedures. Remove the collet and check it for dirt, metal chips, corrosion, or visible wear. Clean the collet, spindle taper, chuck, and test bar carefully.
Even a tiny chip trapped between two mating surfaces can affect the alignment and give you an incorrect reading. Take a little extra time during cleaning, as this simple step can prevent unnecessary troubleshooting later.
2. Install the Collet Properly
Once everything is clean, install the collet according to the manufacturer's instructions. Insert the test bar to the appropriate depth and tighten the assembly using the recommended method.
Avoid uneven tightening or using an incompatible collet. Both can affect how securely the test bar sits in the chuck. A properly fitted CNC collet chuck helps provide consistent clamping and supports accurate measurements.
3. Set Up the Dial Indicator
Attach the dial indicator to a stable stand so it does not move during testing. Place the indicator tip against the test bar, keeping it approximately perpendicular to the surface being measured.
Apply the recommended preload and check that the indicator moves freely. A loose stand or incorrect contact angle can affect the readings, so make sure everything is secure before proceeding.
4. Rotate the Spindle Manually
With the machine stopped, rotate the spindle manually if the equipment permits it safely. Watch the dial indicator as the test bar completes one full revolution.
Note the highest and lowest readings displayed on the dial. Never attempt to adjust the indicator or touch rotating components while the machine is running. Follow the machine manufacturer's safety instructions throughout the process.
5. Calculate the Total Indicated Runout
Calculating TIR is simple. Subtract the lowest reading from the highest reading.
For example:
- Highest dial reading: 0.012 mm
- Lowest dial reading: 0.004 mm
- Total indicated runout: 0.008 mm
The measured runout is therefore 0.008 mm, or 8 micrometres. Whether this is acceptable depends on the machine, tooling, workpiece, and required machining tolerance. Always compare the result with the relevant specifications.
6. Take Measurements at Different Points
Do not rely on just one measurement if you want a clearer picture of the setup's condition. Check the test bar near the collet and then measure it farther along its length.
If the reading changes significantly between these positions, the problem could involve angular misalignment, a bent test bar, or an issue with the spindle or chuck. Repeat the test after checking each component to help identify the actual cause.
How Collet Quality Influences Runout
The quality and condition of a collet can make a real difference to machining accuracy. Worn clamping surfaces, damaged slots, poor fit, and uneven gripping pressure can all contribute to excessive runout.
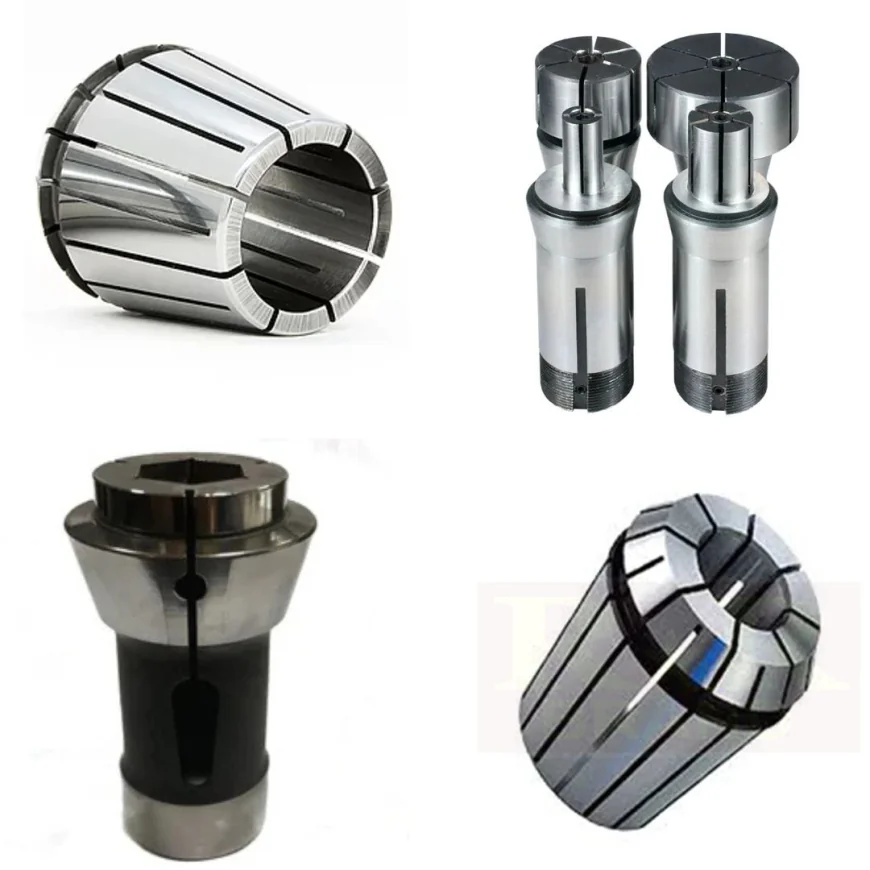
Different machines require different collet designs. For example, Traub collets are used in compatible automatic lathes, while ER collets are widely used for milling, drilling, and other machining operations. DIN 6343 collets are suitable for machines designed for this collet standard.
When choosing a replacement, check the dimensions, clamping range, machine compatibility, and accuracy requirements. Experienced Collet manufacturers can help you find components that match your equipment and application.
Common Mistakes to Avoid
A few simple mistakes can lead to misleading runout readings. Measuring a dirty test bar, using an unstable indicator stand, or tightening the collet incorrectly can affect the results. A bent test bar may also make a properly functioning collet appear faulty.
Always check the measuring equipment and test bar before deciding that the collet needs replacement. If excessive runout continues after cleaning and reinstalling the components, inspect the chuck and spindle for possible damage.
Conclusion
Checking collet runout with a dial indicator is a practical way to identify alignment problems before they affect machining quality. The process involves cleaning the components, fitting the collet correctly, positioning the indicator, recording the readings, and calculating the total indicated runout.
Making this check part of regular machine maintenance can help reduce tool wear, improve surface finish, and maintain consistent production results. With careful measurements and the right collet for your application, you can catch potential problems early and avoid unnecessary machining errors.