Changing a Laser Cell Task Is a Project, Not a Programming Job
Programming is the cheapest part of changing what an automated welding cell does. Fixturing, process re-establishment and revalidation of the tasks the cell already runs are what cost time and money.
 johnmin ren
Changing a Laser Cell's Task Is a Project, Not a Programming Job
Robot cells are sold as flexible. The sales material says flexible, the demonstration shows three variants in an afternoon, and the quotation includes an option for additional part families. Every one of those claims is true and none of them mean what a production engineer assumes they mean on day one.
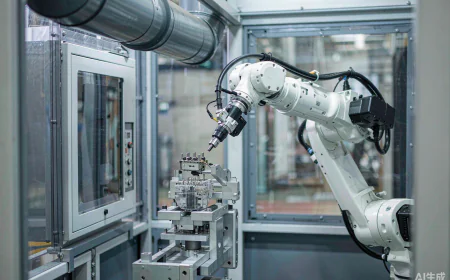
Changing what a laser welding cell is tasked with is a project. The programming is the smallest part of it, and the largest parts are the ones that appear after the first attempt to weld the new part.
What actually has to change
Moving a Laser Welding Cell to a new task involves four categories of change, and programming is the smallest and fastest of them.
Four categories, in the order they bite.
Programming. The taught path, the approach and retreat, the seam geometry. This is the visible part, and it is genuinely quick for a variant within an existing family. A cell taught on one product in a series where the variants differ in a couple of dimensions is programmed in an afternoon. A cell moving to a structurally different component is a different piece of work.
Fixturing. A fixture is not a generic holder; it is a set of locators and clamps designed for one geometry. A new component needs a new fixture, and a fixture is a manufactured item with lead time, machining, and a design cycle that is entirely outside the cell.
Process parameters and tooling. The parameter set for one joint is not the parameter set for another. Different materials, thicknesses, and joint configurations need different settings, different consumables, and often different optical tooling. The source and the focusing arrangement are part of this category and are frequently the constraint that decides which tasks the cell can take at all.
Verification. A new task means a new first article, which means a new process window, a new parameter record, and a new conformance record. This is the step that is routinely omitted because it feels administrative, and it is the one that determines whether the new task is actually running or merely running.
The variation question, which is the one that matters
The genuinely expensive capability is not a new part. It is a new variant inside a part family that shares geometry, tooling and process.
The distinction has a concrete test. If both parts can be held by the same fixture with the locators in the same positions, if the joint is the same type and size, and if the parameter set changes only in magnitude rather than in kind, then the variant is a programming task with a parameter table. That is the case where flexibility is real, and the cell will handle a surprising number of variants in it.
If the new part needs different locators, a different joint configuration, or different optical tooling, then it is a new task and it is quoted as one. A supplier who says a cell is flexible and then quotes a day for a variant that falls outside the shared-fixture case is not being unreasonable; they are telling you the fixture has to be remade and the parameter window re-established.
The useful question when a new task arrives is therefore narrow and concrete: does this share the fixture and the joint, or does it not. Everything else follows from the answer.
Cost structure, stated honestly
Three cost buckets, and the ratio between them is not what people expect.
Programming is the cheapest and is quoted by the hour. A variant inside the shared-fixture case is a few hours.
Fixturing is the dominant cost for a new geometry and has the longest lead time, because a fixture is designed, machined, proven, and then proven again against the part. This is where the schedule risk sits, and it is invisible in a cell quotation.
Process re-establishment sits between them and is the item most likely to be underquoted, because a supplier who has done it before knows it takes a week and a supplier who has not will quote it as a short trial. This is the item worth asking about specifically, and the answer to give is the window width achieved on the last new task.
What to put in the automation quotation
Five items that turn a flexibility claim into a specification.
- A named variant list, with each variant classified as inside or outside the shared-fixture case. Not a capability statement; a list.
- The fixture architecture described honestly. Whether fixtures are dedicated per part or shared across a family, and what a changeover involves physically.
- Changeover time, measured for one variant inside the family case, and stated for the outside case as a project with a lead time rather than a day.
- Process parameter management — how many parameter sets the controller holds, how they are versioned, and who can change them. This is what determines whether adding a variant degrades the consistency of the existing ones.
- What happens to the original task. When a cell takes on a new variant, the original programme keeps running. The revalidation burden of that coexistence is real and it is usually not discussed.
The revalidation trap
This is where a genuinely flexible cell surprises people: a Laser Welding Cell absorbing new variants pays for the gain with revalidation on the tasks it already runs.
One consequence deserves stating on its own because it is the most common source of surprise in a cell that is genuinely flexible.
Adding a parameter set to a controller is trivial. Adding it correctly is not, because the process on the existing tasks can be affected by shared resources: the same source, the same gas supply, the same extraction, the same fixture family. A change that should be isolated in principle is coupled in practice.
The consequence is that a flexibility gain on one side of the cell is paid for with a revalidation on the other. If the cell runs two part families and one of them changes, the other one needs evidence that it still runs. That evidence costs engineering time, and on a production programme it is rarely budgeted because nobody on the operations side knows it exists.
The mitigation is procedural and cheap: require revalidation of the unaffected tasks whenever a shared resource or a shared fixture family is touched, and put it in the change control procedure rather than discovering it as a surprise. It is a paragraph in the change management section, and it prevents an argument that otherwise happens at the worst possible moment.
When flexibility is genuinely the deciding factor
It is worth being clear that this is a real capability and not a sales artefact, because a Laser Welding Cell specified for a switch component family genuinely can absorb variants.
The case where flexibility justifies the investment is a product family with a high variant count and a stable core geometry. That is a common situation in electrical components, and it is exactly the situation where a dedicated cell pays back over its life rather than in its first year.
The case where it does not is a single product with occasional engineering changes. That is a cell that will be revalidated more often than it will be reprogrammed, and the economics are not attractive.
The question to ask the supplier, then, is not whether the cell is flexible. It is which of your variants sit inside the shared-fixture case, and what did the last new one cost. The answer tells you whether the flexibility is a capability you have or a phrase in a brochure, and it is answerable in a sentence by anyone who has actually configured cells for your product.