7 Key Benefits of Using a Roll Compactor in the Pharmaceutical Industry
Learn why roll compactors beat wet granulation: no moisture or heat exposure, fewer steps, better powder flow, less waste, and consistent tablet quality.
 Riddhi Pharma Machinery
Introduction
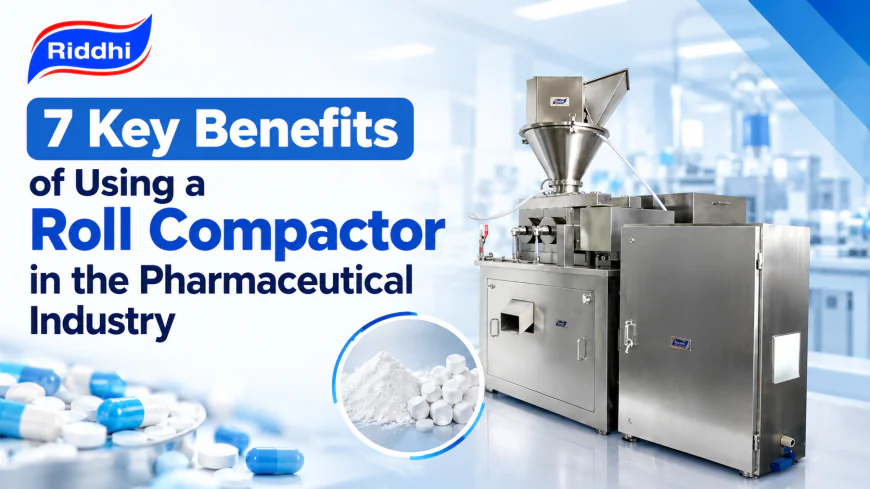
A Roll Compactor is a piece of pharmaceutical processing equipment that turns loose powder into dense, compact granules without using any liquid or heat. It works using two rollers that rotate in opposite directions, squeezing powder between them under mechanical pressure until it forms a solid ribbon. That ribbon then gets milled down into granules, ready to be compressed into tablets or filled into capsules. The entire process stays dry from beginning to end, which is exactly why it's called dry granulation.
This is important in pharmaceutical manufacturing because not every active ingredient can handle the wet granulation process that's traditionally used to prepare powders for tabletting. Some compounds degrade when exposed to moisture. Others break down under the heat needed to dry a wet granulate afterward. A roll compactor avoids both of these risks entirely, which is why it's become a standard piece of equipment for manufacturers working with sensitive formulations.
Beyond protecting fragile active ingredients, roll compaction brings a handful of other advantages that matter across production: better powder flow, less material waste, fewer processing steps, and more consistent tablets from batch to batch. This article discusses each of these seven benefits in detail, so you can see exactly why roll compaction is used in modern pharmaceutical manufacturing.
Where a Roll Compactor Makes a Difference
Switching from wet to dry granulation has a major impact on production. It changes how the batch reacts at every stage, from how the powder handles at the start to how consistent the finished tablets turn out at the end. Here's where that difference actually shows up:
1. No Moisture Exposure for Sensitive APIs
Wet granulation depends on a liquid binder to hold powder particles together. That's fine for a stable compound, but it's a major problem for an active ingredient that degrades, or worse, forms a toxic impurity, the moment it comes into contact with water. Roll compaction sidesteps this completely, since there's no liquid step in the process at all.
The powder goes in dry and comes out as a compacted ribbon, still dry. No solvent, no aqueous binder, nothing that could react with a moisture-sensitive compound along the way. For a lot of formulations built around fragile APIs, this isn't just a nice feature to have; it's the reason roll compactor gets chosen in the first place. Some active ingredients simply can't be run through a wet process without losing potency or picking up degradation products that show up later in stability testing.
2. No Drying Stage Needed
Here's the thing about wet granulation that doesn't always get enough attention: it's not just the water that's the problem; it's what happens to get rid of it afterward. Once the granules are wet, they need to be dried, and that drying step exposes the material to heat, sometimes for a fairly extended period depending on batch size and equipment.
For a heat-sensitive compound, that's a second exposure risk stacked right on top of the first one. A roll compactor removes this stage entirely, because there was never any liquid to dry off. The powder gets compacted, milled, and moves on, without ever seeing an oven or a fluid bed dryer. That is very important since a compound that survives moisture exposure might still degrade under the heat needed to dry it out afterward.
3. Fewer Processing Steps and Faster Turnaround
Every extra step in a manufacturing process costs something: time, labour, equipment cleaning, and another point where a batch could go wrong. Wet granulation typically runs through mixing, wet massing, drying, and then milling, four distinct stages before the granules are even ready. Roll compaction condenses that down to two: compact, then mill.
That difference adds up fast across a production schedule. Shorter batch cycles in the roll compactor mean more throughput without adding shifts or equipment. Less handling means fewer opportunities for the material to pick up contamination or for something to go slightly wrong between stages. And with fewer equipment changeovers, the cleaning and validation burden that comes with each transition shrinks too, which isn't a small thing in a regulated manufacturing environment where every changeover needs documentation.
4. Better Powder Flow and Compressibility
Anyone who's watched fine powder bridge up in a hopper instead of flowing smoothly into a tablet press knows how much of a problem this can become. Cohesive, fine powders tend to clump, stick to surfaces, and flow inconsistently, and that inconsistency shows up as variation in the finished tablet.
Roll compactor fixes this at the source. Pressing the powder into dense ribbons and then milling it into granules increases bulk density and dramatically improves how freely the material flows. Granulated material moves through a hopper and fills a die cavity in a much more predictable way than loose powder ever does, and that predictability is exactly what keeps tablet weight consistent from one tablet to the next. Regulatory bodies pay close attention to weight variation for good reason, since it's a direct proxy for whether patients are getting a consistent dose.
5. Less Raw Material Waste
Active pharmaceutical ingredients aren't cheap, and in a lot of formulations, the API is by far the most expensive component in the whole batch. Any process that wastes less of it has a major and measurable impact on production cost, not just a theoretical one.
Roll compactor tends to waste less material than wet granulation, mainly because there's no liquid binder to account for and less product left clinging to equipment surfaces during a wet massing step. It's a small efficiency gain on any single batch, but it compounds. Run the same formulation a hundred times over a year, and the savings from reduced material loss start to look a lot more significant than they did on paper for one batch.
6. Supports Continuous, Scalable Production
Pharmaceutical manufacturing has been moving toward continuous production for a while now, and roll compaction fits that shift far more naturally than wet granulation does. The reason comes back to the drying stage again, or rather, the absence of one.
Wet granulation is inherently batch-based, since drying happens in cycles and forces a stop-start rhythm on the whole process. A roll compactor doesn't have that constraint. Powder can move through compaction and milling in a continuous stream, which gives manufacturers more predictable throughput and an easier path when scaling up from a small lab batch to full commercial volume. Formulations that work one way at lab scale and differently at production scale are a known problem in pharma, and roll compaction tends to scale more consistently than wet processes typically do.
7. More Consistent Tablet Quality Batch to Batch
At the end of the day, consistency is the whole point of pharmaceutical manufacturing. A patient taking their tenth refill needs the same dose they got on their first, not something that drifted slightly because one batch was processed a little differently than another.
A Roll compactor, with its controlled pressure and a defined ribbon thickness that can be tightly monitored, produces granules with far more predictable density and particle size distribution than wet granulation methods tend to. Wet granulation carries more variables: how much liquid was added, how long the drying ran, how evenly the heat distributed through the bed, and each of those variables is a place where batch-to-batch consistency can slip. Fewer variables generally mean tighter control, and tighter control shows up in the finished tablet as more consistent hardness, disintegration time, and dosage uniformity.
Conclusion
A roll compactor solves what wet granulation simply can't, which is protecting moisture- and heat-sensitive APIs while producing granules that flow well and compress into consistent tablets. Riddhi Pharma Machinery Ltd. manufactures these compactors built around exactly these needs, giving pharmaceutical manufacturers a reliable way to granulate difficult formulations without compromising stability. Get the process right, and you're not just saving time on the production line; you're protecting the one thing that matters the most: the active ingredient your patients depend on.
FAQs
Q. What's the main difference between roll compactor and wet granulation?
Ans. Roll compaction uses mechanical pressure to compress powder into ribbons without any liquid binder, while wet granulation uses a liquid to bind powder particles together before drying. Roll compaction avoids the moisture and heat exposure that wet granulation requires.
Q. Is roll compaction suitable for all pharmaceutical formulations?
Ans. No, roll compaction is not always suitable for all pharmaceutical formulations. It works particularly well for moisture-sensitive and heat-sensitive active ingredients, but some formulations are better suited to wet granulation depending on their specific compaction and flow properties. Testing at a small scale usually confirms which method fits a given formulation.
Q. Does roll compactor affect how quickly a tablet dissolves?
Ans. Yes, it can affect how fast a tablet dissolves. Since roll compaction produces denser granules than some wet granulation methods, which occasionally affect disintegration time. This is why formulation and process parameters need careful control to hit the required dissolution profile for a specific drug product.
Q. Can roll compaction be scaled up from small lab batches to full production volume?
Ans. Yes, and it generally scales more predictably than wet granulation, since the process doesn't rely on drying conditions that can react differently at different batch sizes. This makes it a practical choice for manufacturers planning to scale from development to commercial production.
Q. How does roll compaction improve tablet weight consistency?
Ans. Better powder flow from the granulation process means more consistent filling of the tablet press die cavity, which directly reduces weight variation between individual tablets, an important factor in meeting regulatory content uniformity requirements.
Q. Does using a roll compactor reduce overall production time compared to wet granulation?
Ans. Generally, yes, since it removes the drying stage entirely and reduces the total number of processing steps. This shortens batch cycle time and reduces the handling and equipment changeovers that wet granulation typically requires.