AZ80A vs AZ61A Magnesium Alloy: Strength, Formability and Applications
Compare AZ80A and AZ61A magnesium alloy for extrusion and forging strength, formability, machining, applications, and material selection.
 李志文
Choosing Between AZ80A and AZ61A for a Wrought Magnesium Part

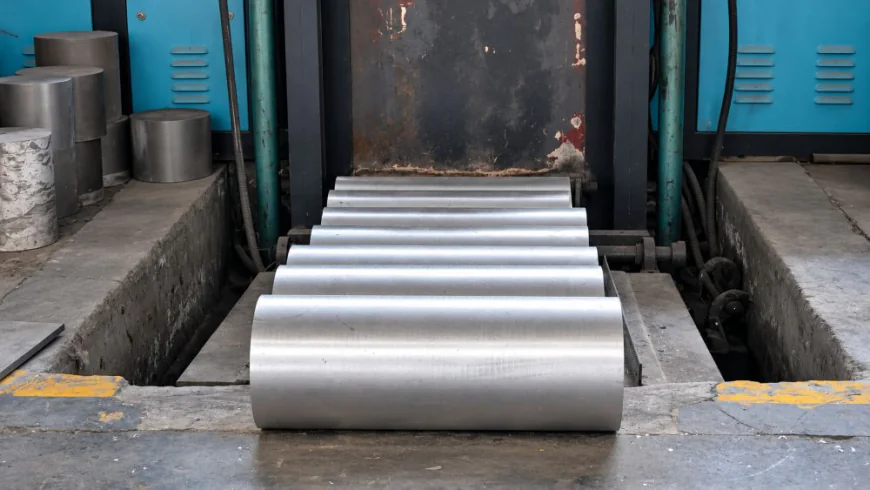
AZ80A and AZ61A are often compared when a magnesium extrusion or forging needs more strength than a basic sheet alloy can offer. The usual split is fairly clear: AZ80A is considered when the load case is demanding and extra strength is worth a more controlled production route. AZ61A is often easier to work with when the profile still needs bending, straightening, or other secondary operations.
The alloy label alone does not settle the job. A buyer may see a stronger AZ80A data-sheet number and assume it is the automatic upgrade. That can be expensive if the part still has to be formed after extrusion, or if the supplier needs extra development to keep a thin profile straight.
In a common solid-extrusion reference, AZ61A-F is listed at 275 MPa ultimate tensile strength, 150 MPa yield strength, and 7% elongation. AZ80A-T5 is listed at 310 MPa, 205 MPa, and 2% elongation. Those figures show the tradeoff: AZ80A-T5 brings more strength, while AZ61A keeps more stretch. They are useful for early screening, but the final numbers must match the specified form, temper, direction, and material standard.
That distinction shows up in everyday design work. A compact bracket with a well-defined load path may benefit from AZ80A. A long rail with local bends, a tube that needs end forming, or an extrusion likely to need straightening can be a better match for AZ61A. Geometry matters just as much as the alloy. One thick section beside several thin webs can make either grade difficult to extrude and hard to hold during machining.
The manufacturing sequence deserves attention before the material is released. Magnesium machines well, but a thin wall can move when clamps come off or when a deep pocket removes residual stress. Coating, fastener isolation, and corrosion exposure should also be part of the discussion. Bare magnesium beside dissimilar metals in a wet environment is not a detail to leave for the end of the project.
For a clean quotation, send the 2D drawing and 3D model, identify the product form, and call out the temper, flatness, critical surfaces, coating, inspection needs, and expected quantity. That gives a supplier something real to price instead of asking them to guess at the production route.
For a closer comparison of material condition, forming, machining, and sourcing, see this AZ80A vs AZ61A magnesium alloy guide.