AZ80A-T5 vs AZ80A-T6: Properties and Heat Treatment
Compare AZ80A-T5 and AZ80A-T6 by heat-treatment route, forged-part properties, distortion risk, machining sequence, and purchase-order callouts.
 李志文
Why AZ80A Temper Choice Can Change a Forging Program

On many drawings, the difference between AZ80A-T5 and AZ80A-T6 is one character. On the shop floor, it can mean another furnace cycle, a quench step, more handling, and a different plan for final machining.
Both conditions are artificially aged, but they arrive there by different routes. T5 is associated with cooling from the elevated fabrication process and then aging the material. T6 adds solution heat treatment and quenching before aging. That extra cycle may be required by a particular specification or qualified component program. It should not be treated as an automatic upgrade simply because the number is higher.
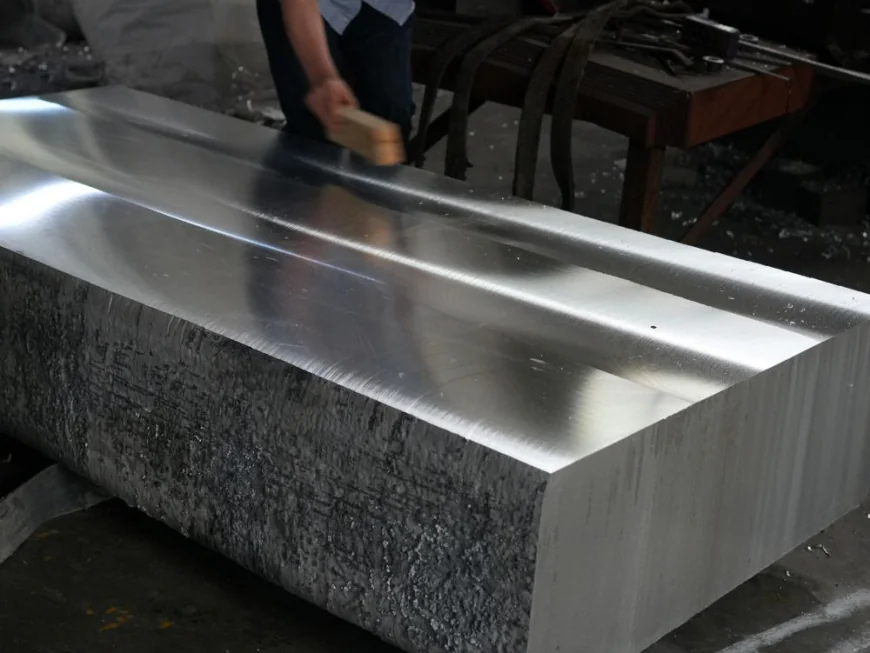
For an AZ80A forging, the geometry is part of the decision. A compact, thick section may move very little through a solution-treatment route. A part with thin ears, open ribs, or a wide machined pad may be more sensitive. If the final bore, sealing face, or mounting surface is machined before the last heat-treatment cycle, the supplier needs to allow for any movement afterward. Often the safer route is to leave stock, complete the required thermal work, and finish the critical features once the part has settled.
Published research on AZ80A model forgings shows why the details matter. In one study, forgings made at 400°C and processed to T5 reached 366 MPa ultimate tensile strength and 293 MPa yield strength. Comparable T6 specimens in the same study reached 333 MPa and 241 MPa. Those are not blanket values for every purchase order, but they show that a T6 route does not automatically produce the stronger result. Forging temperature, solution treatment, aging practice, grain structure, and the part form all play a role.
The quote package should identify the material standard, product form, required temper, certification needs, and the features that control assembly. It also helps to state whether flatness is judged in the free state or while supported. That one note can prevent an argument after the first parts leave the fixture.
For buyers, the practical question is whether the requested condition is already supported by the supplier’s qualified route. If it is not, there may be added trials, lead time, inspection, or machining allowance. Those are details worth knowing before the forging dies are committed.
For a closer look at AZ80A-T5 and AZ80A-T6 properties, heat-treatment flow, and machining implications, read this AZ80A temper comparison guide.